Conveyor Belt Production Line Exporter Guide to Reliable Supply Chains
2026-10-15
Finding a conveyor belt production line exporter who won't disrupt your schedule is harder than it should be. One missed shipment or substandard component can stall an entire plant. That's why this guide focuses on supply chain fundamentals—and why SFC treats every order as a test of trust. In the sections ahead, you'll learn how to assess lead times, quality control, and after-sales support before making a commitment.
Why Conveyor Belt Exporters Can't Afford a Fragile Production Line
Every stalled conveyor on an export floor doesn't just delay a single shift. It backs up the entire logistics chain, from raw material intake to final container loading. For buyers in overseas markets, the tolerance for missed delivery windows is nearly zero. A belt that snaps under rated tension, delaminates in humid coastal storage, or wears unevenly after two months of abrasive ore means one thing: your shipment isn't leaving on time. And once an importer loses confidence in your reliability, replacing that partnership takes far longer than fixing a splice.
The hidden cost shows up in places accountants rarely look. A fragile line forces you to overstock spare belts, assign extra maintenance crews at night, and reroute production during emergency repairs. Those expenses quietly erode the price advantage you originally quoted to win the export contract. Meanwhile, competitors with a rugged, high-splice-strength belt are running three shifts without unplanned stops. Their per-ton operating cost drops, and they start undercutting your quote on the next tender. You're not just paying for repairs; you're paying for lost bids you'll never see.
Durability isn't a feature to list on a datasheet—it's the reason your export invoices get paid on time. Buyers in mining, agriculture, and port logistics often run conveyors in extreme conditions: scorching ambient heat, salt spray, sharp aggregate, and long idle periods between cargo waves. A belt built with UV-stabilized covers, high-adhesion rubber, and reinforced carcass layers doesn't just survive; it keeps tension stable across temperature swings and resists edge fraying during misalignment. When you ship a line that can be installed and forgotten for a year, your buyers remember that. They reorder. They refer you to their subsidiary in another continent. Fragility might save you a few dollars per meter at the factory gate, but it costs you the lifetime value of the customer.
The Three-Minute Factory Walkthrough That Separates Reliable Suppliers
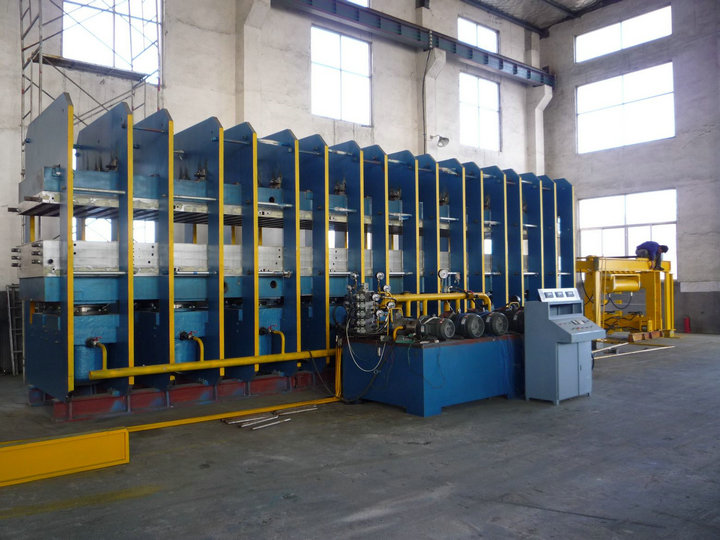
Walk past the receiving dock and ignore what the tour guide is saying for a minute. Watch how incoming material moves. In a dependable plant, boxes get opened near the point of use, not piled in a corner to be sorted later. If you see staff walking back and forth without carrying anything, that's a signal: motion without material is wasted time, and it usually shows up later as missed delivery dates.
Spend another sixty seconds near the line where the actual assembly or packing happens. Reliable suppliers tend to have short visual cues—color-coded bins, chalk marks on the floor, a board with today's target and current count. You're not looking for polish. You're looking for whether the person doing the job can tell you, without checking a computer, whether they're ahead or behind. When they can, schedules aren't guesswork.
Before you leave, glance at the maintenance corner. A five-year-old machine with clean grease points and a handwritten log beats a brand-new line that's already covered in tape and temporary fixes. Reliable suppliers don't hide problems; they mark them and assign a date. That level of honesty shows up in every shipment.
Material Sourcing Without the Guesswork
Nothing slows down production like a supplier who promises one lead time and delivers another. Real material sourcing without guesswork starts by replacing vague assurances with hard numbers—actual on-time rates, rejection percentages, and recovery times from past disruptions. Those figures tell you which vendors are reliable under pressure, not just on paper.
The second piece is building a short list of approved materials with clear substitution paths. When a primary component goes short, teams waste days asking around whether an alternative will hold up. Instead, pre-test and pre-approve two or three fallback options for every critical input, with documented performance data. That way, a shortage triggers a decision already made, not a fresh round of calls and hope.
Finally, treat cost as a range, not a single quote. Markets move, freight shifts, and tariffs change. A sourcing plan that includes best-case, likely, and worst-case landed costs lets you see where real exposure sits and adjust orders before a surprise becomes a line-down event.
Quality Gates That Catch Defects Before They Exit the Plant
A quality gate is only as strong as the people who stand behind it. On the line, inspectors don't just check boxes—they feel for burrs, listen for rattles, and trust the faint smell of overheated adhesive that no camera can catch. The best gates are placed where a mistake is cheapest to fix: right after a critical torque, before a cosmetic panel goes on, or just before the final packaging. When a defect slips past, the cost multiplies tenfold down the line, so these checkpoints are designed to be impossible to ignore without a deliberate choice.
We learned early that a gate with a pass/fail light is not enough. Operators need to know why something failed and what to do next. That's why each station has a simple board with the top three defects from the past week, written in marker, not printed from a database. If a hinge squeaks, the fix is a drop of oil and a note to the supplier—not a form in triplicate. The goal is to catch the defect before the part leaves the cell, and to make the correction so natural that it becomes part of the rhythm.
Some plants over-engineer their gates with vision systems and torque transducers on every bolt. We found that a human hand with a feeler gauge and a mirror beats a camera when it comes to a scratch inside a bore. The key is to keep the gate close to the work, not at the end of the line where rework means tearing down a finished product. A good gate is boring: it never lets a bad part through, but it also never stops a good one. That's the difference between inspection and policing—one builds trust, the other builds a backlog.
Logistics Partners Who Treat Your Conveyor Line Like Their Own
A good logistics partner doesn't just clock in and out around your conveyor line—they notice the small stuff before it becomes a shutdown. That means checking belt tension, listening for bearing noise, and tracking wear patterns like it's their own equipment on the line.
You'll see it in the way they carry spare parts, mark a questionable sensor, and leave the work area cleaner than they found it. When a problem does surface, they don't wait for a work order. They flag it, suggest a fix, and often have the tools already in hand. That level of care comes from experience and a real sense of accountability, not from a checklist.
Over time, that kind of ownership shows up in fewer surprise breakdowns, longer stretches between repairs, and a line that keeps moving without constant oversight. It's the difference between hiring a vendor and gaining a crew that treats your operation like it's their name on the building.
Planning for the Port Delay You Haven't Met Yet
A port delay you haven't met yet rarely announces itself. It may come as a quiet customs hold in Rotterdam, a sudden equipment shortage in Los Angeles, or a fog bank that closes the Yangtze estuary for two days. The mistake is treating these as anomalies. They are recurring features of ocean freight, and the only way to plan for them is to assume they already exist in your transit time. That means padding schedules not with a fixed percentage, but with scenario-based buffers tied to specific lanes and seasons.
Instead of asking when the cargo will arrive, ask what breaks first if it is five days late. That shifts attention from tracking to response design. Build a small playbook of alternatives before you need them: a shortlist of alternate discharge ports, pre-cleared trucking partners near secondary terminals, and inventory thresholds that trigger air freight for only the most critical SKUs. This kind of pre-negotiation costs little until the day the delay you haven't met becomes the one you're already managing.
Finally, treat every uneventful shipment as data, not proof of safety. Log the near-misses—the vessel that was almost rolled, the berth that was nearly unavailable, the documentation error caught at the last hour. These silent close calls show where your current plan would have failed under slightly worse conditions. Over time, they reveal the true shape of risk in your supply chain, allowing you to adjust lead times and safety stock for the delay you haven't met yet, rather than reacting to it after arrival.
FAQ
Look beyond glossy brochures. Ask for a list of at least five recent installations with contactable references, ideally in your region or a similar climate. Check how quickly they respond when you ask about custom belt widths or motor voltages—not just standard specs. Also review their in-house testing capability: a supplier that can simulate load cycles and tension shifts before shipment is far less likely to ship a line that fails during commissioning.
Request their component sourcing map, not just a final assembly certificate. A reliable exporter will name the motor, gearbox, and PLC brands they use and show backup suppliers for critical parts. Ask for a written commitment on lead time variation—some exporters promise 45 days but quietly slip to 90 when orders spike. A short video tour of their warehouse and queued production slots often reveals more than a quality audit report.
Watch for vague terms like 'standard tolerances' without numbers, or clauses that allow unilateral changes to belt material after payment. Some contracts exclude the control panel software from warranty, which means you could be left with an operating system lockout after a minor fault. Also be wary if the exporter insists on full payment before the factory acceptance test is scheduled—that usually signals cash flow trouble or a rush job.
ISO 9001 is a floor, not a ceiling. Look for CE marking if the line will operate in Europe, and check whether the exporter's welding procedures meet AWS D14.3 or EN 1090 standards for structural steel. For food-grade or high-temperature applications, ask for third-party reports on belt material migration and roller bearing heat ratings. A certification without a recent audit date is not worth much.
Reliable exporters usually keep a staged spare parts kit at a bonded warehouse near your country, not just in their home factory. They assign a named engineer—not a rotating call center—to your project for at least the first year. Unreliable ones often promise 24/7 remote support but cap video diagnostics at 30 minutes and charge extra for English-speaking technicians. Ask for a sample service ticket with actual resolution times.
A trustworthy exporter will ask about your material density, belt speed range, and ambient dust levels before quoting a price. If they agree to any modification without pushing back on your specs, that's a warning sign. Customization should include a documented change control process—otherwise you may receive a 'custom' line that is just a standard frame with different paint. Request a mock-up of the control interface before signing.
Divide the quote into three parts: initial capital, five-year energy consumption, and expected belt replacement intervals. A cheaper line that uses non-standard rollers may cost three times more in maintenance over two years. Ask the exporter to provide a total cost of ownership estimate with assumptions clearly stated. Also compare the cost of a two-day commissioning visit—some exporters hide this until after the deposit is paid.
Many buyers forget to confirm whether the line will be shipped fully assembled or in knock-down kits. Knock-down kits save freight but require precise labeling and a local rigging crew. Check who is responsible for port storage fees if customs clearance is delayed—those charges can exceed the freight cost. Also verify the exporter's packing method for long belt rolls: if they are coiled too tightly, the carcass can develop flat spots before installation.
Conclusion
A conveyor belt export business lives or dies by the strength of its production line, and the first warning sign is usually hidden in plain sight. When a line can't handle minor fluctuations in tension, speed, or raw material variance, the cost shows up not just in downtime but in renegotiated contracts and damaged buyer trust. A quick factory walkthrough tells you more than any certificate: watch how operators respond to a sudden jam, whether splice points are consistent, and whether the belt path stays true under load. If the floor crew can't explain what happens at each checkpoint, that's a red flag no audit report will catch. Materials matter just as much—ask for batch-level traceability on rubber compounds and fabric layers, not just a generic spec sheet. The difference between a belt that lasts three years and one that fails in nine months often starts with a quieter purchasing decision months before the line ever runs.
Quality gates are where export-grade consistency actually happens. You want defect detection built into the line at the tensioning, splicing, and edge-sealing stages, not just a final glance before crating. If a supplier cannot show you a rejected batch from the last quarter, assume they are shipping borderline product. Then move to the logistics side: the best exporters treat your conveyor line as an extension of their own warehouse floor. That means padded steel cradles, moisture barriers, and a carrier who knows the difference between a roll and a pallet. Even with all that, port delays will happen—so plan for the one you haven't met yet by staging buffer inventory near the exit port and locking in alternate routing for at least two choke points. Reliable supply chains are not built on luck; they are built on suppliers who act like the next shipment already has a problem to solve.
Contact Us
Contact Person: Chen Zhengwei
Email: [email protected]
Tel/WhatsApp: +86-13963975727
Website: https://www.sfcrubbermachine.com