Corn Curls Cheetos Chips Extruder Machine Factory Selection and Setup Guide
2026-10-31
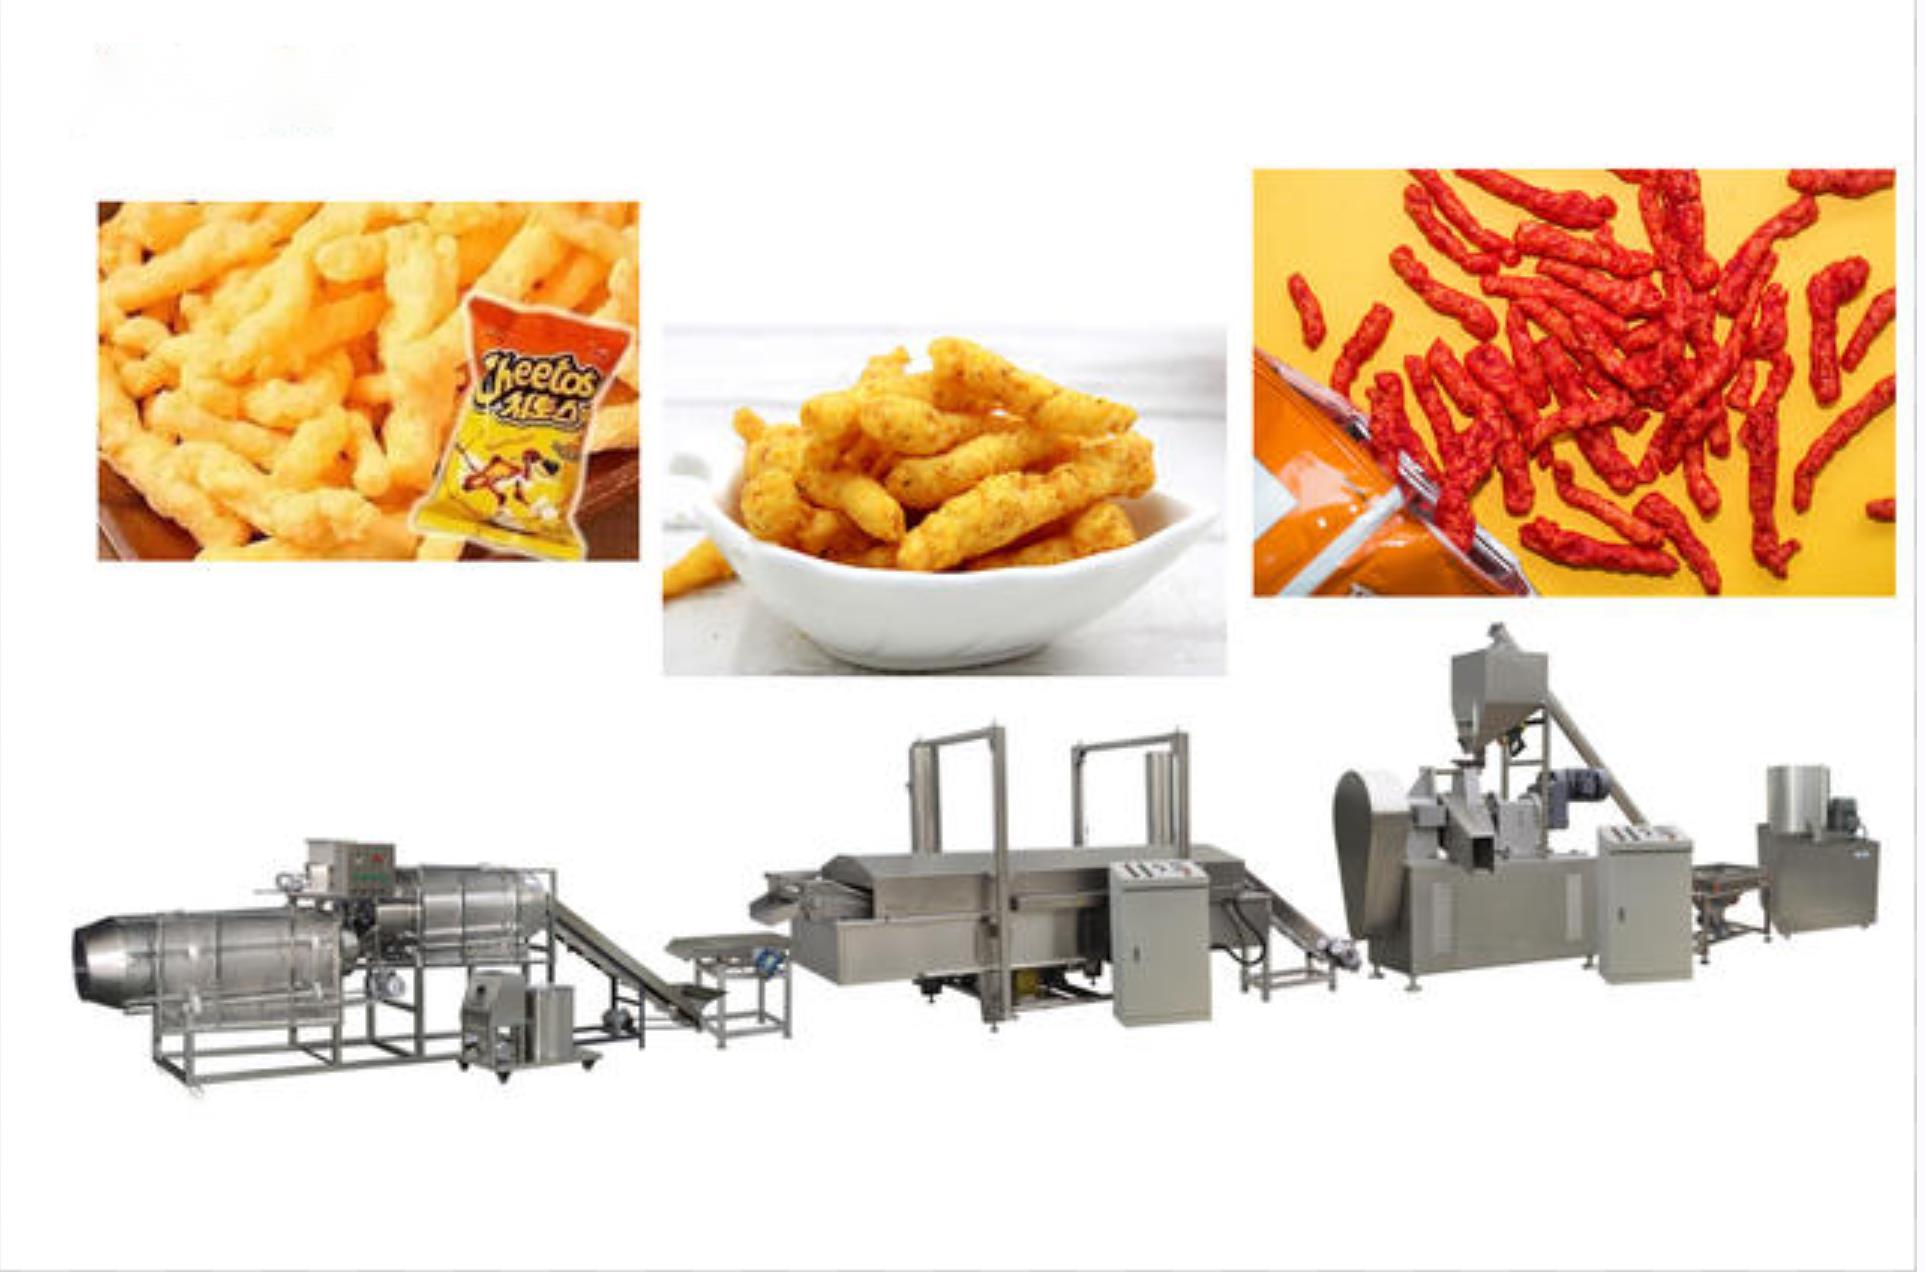
Setting up a production line for corn curls and Cheetos-style chips is rarely as straightforward as the sales brochures suggest. The real bottlenecks—screw configuration, die design, moisture control, and factory support—show up only after the machine is on your floor. That’s why factory selection matters as much as the extruder itself. In this guide, we break down what to look for before you commit, and how working with a partner like MINGDE can help you avoid the setup pitfalls that quietly eat into your margins.
Sizing the Extruder Around Your Daily Corn Curl Output Instead of the Sales Sheet
Most equipment suppliers will hand you a glossy sheet full of impressive throughput numbers, but that rarely matches what actually happens on your floor. The smarter move is to reverse the math: take how many pounds or kilograms of corn curls you genuinely pack out per shift, then add a realistic buffer for startup scrap, flavor changes, and the occasional slow afternoon. An extruder sized for 800 pounds an hour when your real daily output is 600 pounds total is just a costly way to run half-empty barrels and fight moisture swings.
Start with your daily target, not the machine's theoretical maximum. If a full production day means 2,000 pounds of finished curls, work backwards through drying, coating, and packaging losses to see how much raw extrudate you need before the dryer. That number, divided by the hours you actually run—not the hours you wish you ran—gives you a true required rate. Then pick an extruder that sits comfortably in the middle of its range at that rate, so you are not redlining the screw just to hit a normal Tuesday.
Also remember that corn curl density and shape affect how much "output" really means. A light, puffy curl might fill bags quickly but weigh far less per hour than a denser snack. If you size purely by weight from a sales sheet, you could end up with a machine that makes plenty of product but cannot feed your packaging line fast enough. Match the extruder to your daily finished volume, your actual run schedule, and your product's bulk density—then let the sales sheet be a reference, not the rule.
Screw and Barrel Wear Patterns That Reveal a Factory's True Build Quality
A quick glance at the screw flights can tell you more about a machine shop than any glossy brochure ever will. Uniform, shallow wear along the pushing side of the flight suggests consistent material flow and well-controlled temperatures. But when you spot deep gouges near the feed section or uneven polishing on the barrel wall, that's a red flag. Those patterns usually mean the factory cut corners on hardening, or they ran the extruder dry during start-up just to hit a delivery date.
Barrel wear is equally telling. A properly built barrel should show a gradual, almost mirror-like smoothing from the feed throat to the metering zone. If you see chatter marks or wavy scoring that repeats every few inches, the boring process likely lacked rigidity, or the operators ignored alignment during assembly. Real build quality shows up in how the wear spreads across the full length, not in how shiny the barrel looks on the outside.
Pay attention to the root diameter of the screw too. Factories that prioritize longevity typically grind the root with a slight taper to handle compression without stress risers. When you find sharp steps or inconsistent root depth, you're looking at a rushed job where the engineering was secondary to throughput numbers. These wear signatures stick around long after the paint has faded, making them one of the most honest indicators of what the factory actually built into the machine.
Factory Floor Checks That Matter More Than a Polished Demo Video
When you visit a supplier's factory, skip the glossy showroom and head straight to the production line. Look at how raw materials are stored — are they off the floor, clearly labeled, and protected from moisture? Check whether workers are using calibrated tools and following the exact same steps you saw in the sample batch. These small, unscripted details tell you far more about daily reliability than any edited video ever could.
Pay attention to the pace of work and the condition of the machinery. A factory that rushes one station but lets another sit idle usually has hidden bottlenecks. Ask the line supervisor to walk you through a recent quality issue and show the corrective action log. If they hesitate or give you a vague answer, that's a red flag no marketing material can cover up.
Finally, talk to the people doing the actual assembly. Ask them how long they've been on this line and what they do when something doesn't fit right. Their comfort in explaining the process — and their willingness to point out a defect — is the real proof of a solid quality system. A demo video can be rehearsed; a live floor conversation cannot.
Electrical Load, Water Pressure, and Floor Space Before You Sign
Before you commit to a lease, take a hard look at the building's electrical capacity. Older properties often hide outdated panels that can't handle modern equipment, from commercial kitchen appliances to a full rack of servers. Ask for the panel's amperage and whether any recent upgrades were done—if the landlord hesitates, that's a signal to dig deeper. A simple walk-through with a plug-in tester only tells you if outlets are wired correctly, not if you can run three heavy machines at once without tripping a breaker.
Water pressure is another silent deal-breaker. Turn on every tap, flush every toilet, and if possible, run two fixtures at the same time. Low pressure in an upper-floor unit may point to aging pipes or a shared line that drops when neighbors are active. For businesses that rely on washing, cooling, or food prep, even a modest drop in flow can stall operations daily. Don't accept a vague 'it gets better in the morning'—ask for a pressure test result or bring a small gauge yourself.
Finally, measure the actual usable floor space, not just what's listed in the ad. Columns, odd corners, and unusable nooks eat into your layout faster than you'd expect. Bring a laser measurer and sketch a rough floor plan on the spot. Check ceiling height too, especially if you need storage racks or ventilation ducts. A space that looks generous in photos can shrink by 20% once you subtract dead zones, so confirm that your desks, shelving, or machinery will fit with room to walk and meet code.
Training Operators to Handle Dough Viscosity Shifts Without Stopping the Line
Dough viscosity rarely shifts without warning. Operators trained to read the subtle signals—a slight darkening of the dough surface, a change in the sound of the mixer motor, or a two-degree rise in dough temperature—can often catch a viscosity drift before it disrupts the line. Instead of waiting for a sensor alarm, they use tactile checks: pinching a small dough sample between thumb and forefinger, feeling how quickly it springs back, or pulling a thin strand to judge extensibility. This hands-on calibration turns viscosity management into a continuous, low-tech feedback loop that runs alongside any automated system.
The real skill lies in making small, reversible adjustments without halting production. For instance, if the dough is trending stickier than the target profile, a trained operator might tweak the water feed by a fraction of a percent, adjust the mixer speed by a few RPM, or briefly open a bypass valve to introduce a pre-hydrated flour blend. Each adjustment is logged against the measured viscosity curve, so the team builds a living playbook of cause-and-effect for their specific line, flour lot, and ambient conditions. Newer operators practice these moves on a shadow line or with a simulator that replays real shift data, so their first real-time correction isn't a guess.
Cross-shift communication makes the training stick. Instead of vague notes like "dough was off," operators record specific observations: "viscosity rose 15% after 2 a.m. due to cooler flour room; increased mixer speed from 42 to 45 RPM and reduced water by 0.3% for 20 minutes; line speed never dropped below 92%." This level of detail turns individual adjustments into team knowledge, and it keeps everyone focused on the goal: steady output, consistent product, and no unplanned stops.
Spare Parts Inventory for Day One Without Overbuying
A day-one spare parts shelf should look thin, not "fully stocked." The goal is to cover the handful of failures that will actually stop you in the first month, not to replicate a distributor's catalog. Go through each critical asset and ask one question: if this part fails tonight, can we get a replacement before the line loses more money than the part costs? If yes, leave it off the shelf. If no, it earns a spot.
For quantities, one or two units are usually plenty. Base that on failure history or the manual's wear items, not on a sales rep's suggestion. Keep a simple log of what gets pulled and why. After 60 days, any item still sitting in its box either gets returned if possible or marked as "only if lead time jumps." That keeps your initial spend in check and makes the first reorder cycle much easier to justify.
FAQ
Look beyond glossy brochures. Ask for real production videos, a list of existing clients making similar snacks, and whether they can run a trial with your own corn meal before you commit. A video call tour of their assembly area and quality control also reveals a lot.
A compact line with mixer, extruder, fryer or oven, and seasoning drum can fit in roughly 200 to 300 square meters, but you will want extra room for raw material storage, packaging, and staff movement. If you add a flavoring system and cooling conveyor, plan for at least 400 square meters.
Not automatically. The extruder itself is usually flexible, but the downstream equipment differs. Fried curls need a fryer and de-oiling system, while baked or air-puffed curls need a high-temperature oven or puffing chamber. Ask the factory to confirm which configuration matches your texture target.
Most single-screw or twin-screw extruders run best with moisture between 13 percent and 18 percent. Too dry and the barrel will jam or wear quickly; too wet and the curls won't hold their shape. Always run a small batch to dial in moisture for your specific corn meal.
A standard corn curl line usually needs 380V 50Hz three-phase power, but confirm voltage and frequency with the factory before ordering. You will also need compressed air for pneumatic controls, water for mixing, and proper ventilation or exhaust for frying or baking.
Plan for one to two weeks for mechanical installation, electrical hookup, and dry testing. Add another three to five days for trial runs and operator training. Most teams reach stable output within two to three weeks if the factory sends an experienced commissioning engineer.
Entry-level lines often produce 80 to 150 kg of finished curls per hour. Mid-size units can reach 200 to 400 kg per hour, depending on die size, cutter speed, and whether you use a twin-screw extruder. Be wary of factories quoting maximum theoretical output; ask for average sustained output with your recipe.
Start with clean, consistent corn meal and warm up the barrel fully before feeding. Keep die holes uniform and replace worn cutters early. Monitor barrel temperature zones and don't rush the screw speed on day one. Keep a log of settings for each successful batch so you can repeat it.
Conclusion
Sizing the extruder around your actual daily corn curl output—not the peak numbers buried in a sales sheet—prevents buying a machine that either starves for capacity or wastes energy on an oversized motor and barrel. Calculate kilograms per hour against realistic run times, then leave a 15 percent cushion. During factory visits, ask to see screws and barrels pulled from machines that have run at least 3,000 hours. Wear patterns tell the truth: uneven land wear, deep scoring near the feed throat, or chrome flaking indicate poor base steel or rushed heat treatment. A polished demo video cannot hide bearing play, shaft runout, or weld cracks under load, so run the machine with your own raw material and listen for rhythmic knocking at full screw speed.
Before signing, verify electrical load and phase against your panel, confirm sufficient water pressure for barrel cooling and dough conditioning, and map floor space not just for the extruder but for die changes, hopper loading, and ventilation. Once installed, operator training should focus on viscosity shifts rather than memorizing buttons. Corn curl dough can stiffen or slacken from moisture swings, oil addition, or ambient heat; teach operators to adjust water feed and screw speed incrementally without stopping the line, using torque and die pressure as guides. For spare parts, stock only day-one wear items—a spare screw and barrel set, die plates, cutter blades, bearings, thermocouples, and heating bands—along with one set of seals and gaskets. Avoid buying a full rebuild kit; instead, confirm the factory keeps these parts in regional inventory with 48-hour shipping.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/